In the demanding world of industrial extraction and mineral processing, the efficiency of material transport defines the profitability of an entire operation. Mining slurry pumps serve as the critical arteries of these sites, moving abrasive mixtures of water and solids through complex piping systems to ensure continuous production flow. Without high-performance pumping solutions, the transport of heavy ores and tailings would become a logistical bottleneck, leading to costly downtime and operational instability.
The global shift toward deeper mining and the processing of lower-grade ores has intensified the need for equipment that can withstand extreme abrasion and high pressure. Modern industrial standards now demand pumps that not only move massive volumes of slurry but do so with minimal wear and maximum energy efficiency. This evolution has pushed the boundaries of materials science, moving from standard cast irons to advanced high-strength alloys capable of enduring the harshest subterranean environments.
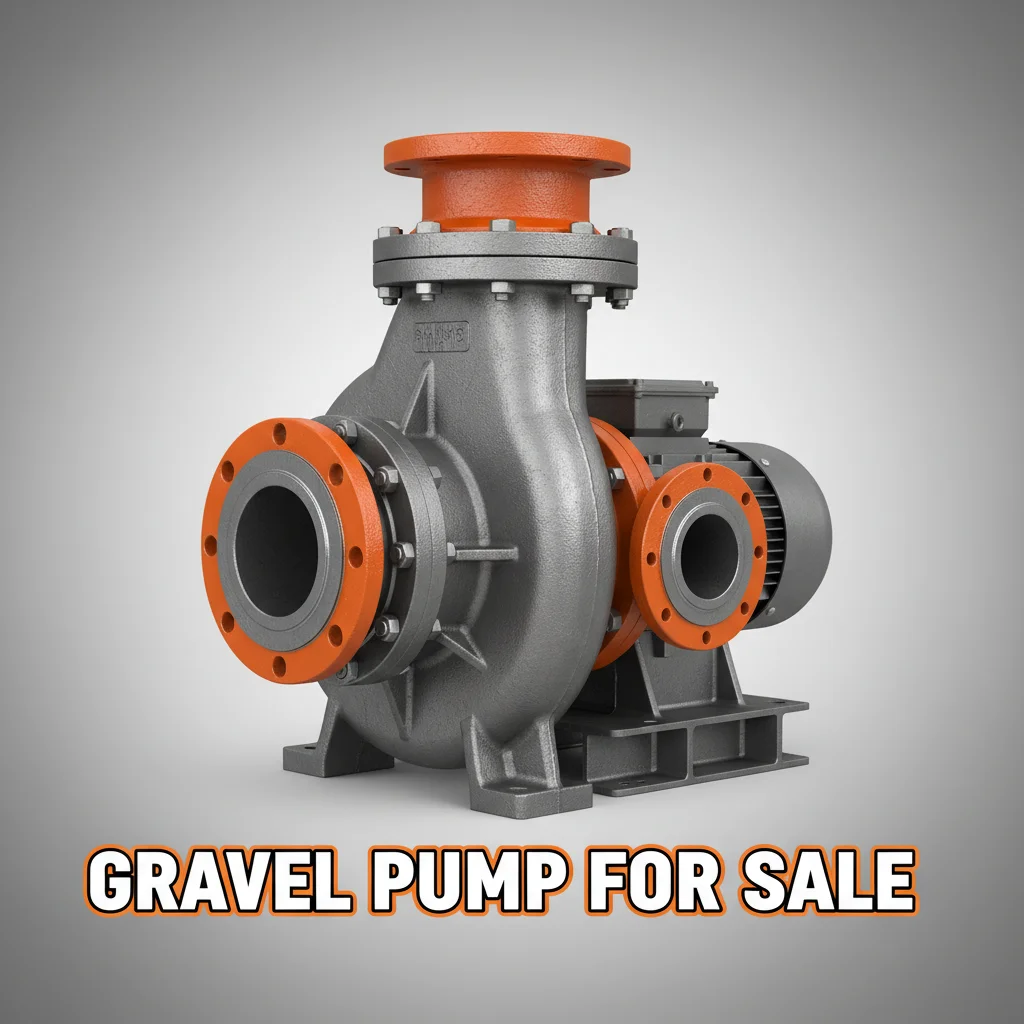
For operators seeking to optimize their dredging and transport workflows, investing in specialized mining slurry pumps is no longer optional but a strategic necessity. By integrating advanced fluid dynamics and wear-resistant engineering, the HWN Series and similar high-capacity systems provide the stability required to handle fluctuating material densities and extreme volumetric demands in large-scale industrial projects.

Global Industrial Context of Slurry Transport
The global mining and dredging sectors are currently facing a critical challenge: the need to process larger volumes of abrasive materials while adhering to stricter environmental and operational costs. According to industrial trends, the demand for efficient solids transport has surged as projects move toward remote, high-pressure environments where equipment failure can lead to millions of dollars in lost revenue.
In this context, the deployment of robust mining slurry pumps has become the primary method for overcoming the friction and wear associated with high-density slurry. By utilizing horizontal cantilever structures, such as those found in the HWN Series, industries can ensure a stable flow of solids even when dealing with particle sizes up to 220mm, maintaining the integrity of the entire processing chain.
Defining High-Performance Mining Slurry Pumps
At its core, a mining slurry pump is a specialized centrifugal machine designed to transport a mixture of liquid and solid particles—known as slurry—without succumbing to rapid internal erosion. Unlike standard water pumps, these machines must manage the extreme kinetic energy of abrasive solids that act like sandpaper against the internal casing and impeller.
Modern industrial dredging pumps, particularly the HWN series, define high performance through a combination of structural integrity and hydraulic efficiency. By employing single or double-pump casings depending on the required capacity (from 200HWN up to 1200HWN), these systems can achieve flowrates as high as 9000 m³/h, making them indispensable for large-scale industrial excavation.
The connection to modern humanitarian and industrial needs is clear: efficient slurry transport is essential for land reclamation, waterway maintenance, and the sustainable extraction of minerals required for the global energy transition. The ability to precisely tune flow rates and head pressure ensures that these pumps can adapt to various site-specific needs, regardless of material density.
Core Engineering Components for Durability
The durability of mining slurry pumps is primarily determined by the material hardness of their internal wear parts. In the HWN series, impellers, sheaths, and liners are forged from high-strength anti-wear alloy cast iron with a hardness exceeding 50 HRC. This ensures that the pump can handle the most aggressive abrasive solids without immediate degradation.
Beyond materials, structural design plays a pivotal role. The use of optimized impeller flow channels reduces turbulence and cavitation, which are the leading causes of premature pump failure. By balancing suction capacity with digging depth, these pumps allow operators to maintain high solids concentrations without risking the stability of the pump casing.
Furthermore, the synchronization of wear cycles is a hallmark of advanced engineering. By designing internal parts to wear at a similar rate, maintenance teams can schedule replacements for the impeller and liner simultaneously. This strategic approach drastically reduces downtime and ensures that the mining slurry pumps maintain peak efficiency throughout their operational life.
Global Applications and Use Case Scenarios
In real-world industrial contexts, these pumping systems are deployed in diverse environments, from deep-sea dredging in Southeast Asia to massive open-pit mine tailings management in Australia and South America. The versatility of the HWN series allows it to be integrated into various configurations, including built-in brackets and integrated gearboxes for OEM requirements.
For example, in large-scale harbor expansion projects, the high flow efficiency of these pumps allows for the rapid displacement of seabed materials. In remote industrial zones where material density fluctuates rapidly, the sharp performance curves of these pumps allow them to adapt instantly, preventing blockages and ensuring a consistent volumetric output.
Operational Efficiency of Different Mining Slurry Pumps Configurations
Long-Term Economic Value and Sustainability
The true value of high-grade mining slurry pumps lies in the reduction of the Total Cost of Ownership (TCO). While the initial investment in anti-wear alloys and reinforced casings may be higher than standard equipment, the extended service life and synchronized wear cycles lead to a dramatic decrease in maintenance frequency and labor costs.
From a sustainability perspective, the high energy efficiency (ranging from 60% to 85%) means lower power consumption per cubic meter of material moved. This not only reduces the carbon footprint of the mining operation but also enhances the overall ROI by maximizing the volume of material displaced per kilowatt-hour of electricity used.
Future Innovations in Pumping Technology
The future of slurry transport is moving toward digital transformation and predictive maintenance. We are seeing the integration of real-time wear monitoring sensors that can alert operators exactly when a liner is reaching its end-of-life, replacing the old method of fixed-interval scheduling with data-driven precision.
Automation is also playing a key role, with variable frequency drives (VFDs) allowing mining slurry pumps to adjust their RPM automatically based on the viscosity of the slurry. This prevents pump overload and ensures that the equipment always operates at its Best Efficiency Point (BEP), regardless of the material's changing characteristics.
Furthermore, the development of nano-composite alloys is expected to push hardness levels even beyond 50 HRC, potentially doubling the life cycles of impellers. These innovations, combined with smarter lubrication systems, will move the industry toward a "zero-unplanned-downtime" operational model.
Technical Challenges and Expert Solutions
One of the most persistent challenges in slurry pumping is cavitation, where low-pressure bubbles form and collapse violently against the impeller, causing pitting and structural failure. Expert solutions involve optimizing the cavitation performance through precise impeller geometry and ensuring that the suction head is perfectly matched to the material's density.
Another common issue is the imbalance between flow rate and head pressure when slurry density changes mid-operation. The HWN series addresses this through a specialized performance curve that drops sharply, providing the flexibility needed to adapt to rapid fluctuations in displacement without losing prime or causing pipe blockages.
Finally, lubrication failure remains a leading cause of bearing collapse. To solve this, modern systems offer a choice between oil and grease lubrication, complemented by automated alerts that remind operators of service intervals, ensuring that the heavy-duty bearings are always protected under extreme load.
Comparison of HWN Series vs. Standard Dredge Pumps
| Feature |
Standard Pumps |
HWN Series Pumps |
Impact on ROI |
| Material Hardness |
Standard Cast Iron |
Anti-wear Alloy (≥50HRC) |
Lower Replacement Cost |
| Wear Life Cycle |
Irregular / Short |
Synchronized / Long |
Reduced Downtime |
| Suction Depth |
Limited |
Enhanced Cavitation Depth |
Greater Operational Range |
| Flow Adaptability |
Fixed Performance |
Dynamic (Speed/Impeller) |
Site-Specific Optimization |
| Casing Design |
Single Wall |
Reinforced Double Casing |
Higher Pressure Tolerance |
| Max Flowrate |
Moderate |
Up to 9000 m³/h |
Higher Volumetric Throughput |
FAQS
The 200-500HWN models utilize a single pump casing, which is ideal for agility and moderate capacities. In contrast, the 600-1200HWN models employ a reinforced double pump casing. This structural upgrade is specifically designed to manage significantly higher volumetric capacities and withstand the extreme operating pressures encountered in large-scale industrial dredging projects.
The HWN series utilizes high-strength anti-wear alloy cast iron for all critical wear parts, including the impeller and liners. With a hardness rating of at least 50HRC, these materials provide a perfect balance of impact resistance and abrasion resistance, ensuring that the internal components can withstand the constant friction of abrasive solids for an extended period.
Yes, the HWN series is designed for high adaptability. Operators can achieve different performance outputs by either adjusting the motor speed via a variable frequency drive or by modifying the diameter of the impeller. This allows the pump to be fine-tuned to match the specific slurry viscosity and displacement requirements of a changing job site.
Depending on the specific model and the operational environment, the HWN series supports either grease lubrication or oil lubrication. Both methods are engineered to provide optimal protection for the bearings during heavy-duty use, preventing overheating and failure even under the high-load conditions typical of mining and dredging.
The HWN series is engineered so that different wear parts, such as the impeller and the liners, reach their replacement cycle at approximately the same time. This synchronization means that maintenance teams only need to shut down the system once to replace all critical components, drastically reducing labor costs and total operational downtime.
A sharp performance curve makes the pump significantly more adaptable to rapid fluctuations in material density and displacement. In active dredging, the concentration of solids can change in seconds; a pump with this characteristic can maintain stability and avoid clogging more effectively than a pump with a flat performance curve.
Conclusion
In summary, the selection of high-performance mining slurry pumps is a cornerstone of operational success in the dredging and mining industries. By prioritizing material hardness, structural integrity through reinforced casings, and hydraulic adaptability, systems like the HWN series solve the age-old problem of abrasive wear while maximizing volumetric efficiency. The transition from standard equipment to synchronized-wear, alloy-based pumping solutions represents a shift toward lower TCO and higher industrial reliability.
Looking forward, the integration of digital monitoring and automated speed control will further refine the efficiency of slurry transport, making it more sustainable and less prone to human error. For companies aiming to scale their operations without increasing their maintenance burden, the focus should remain on investing in equipment that balances raw power with precision engineering. To explore our full range of high-capacity solutions, visit our website: www.hihornpump.com.