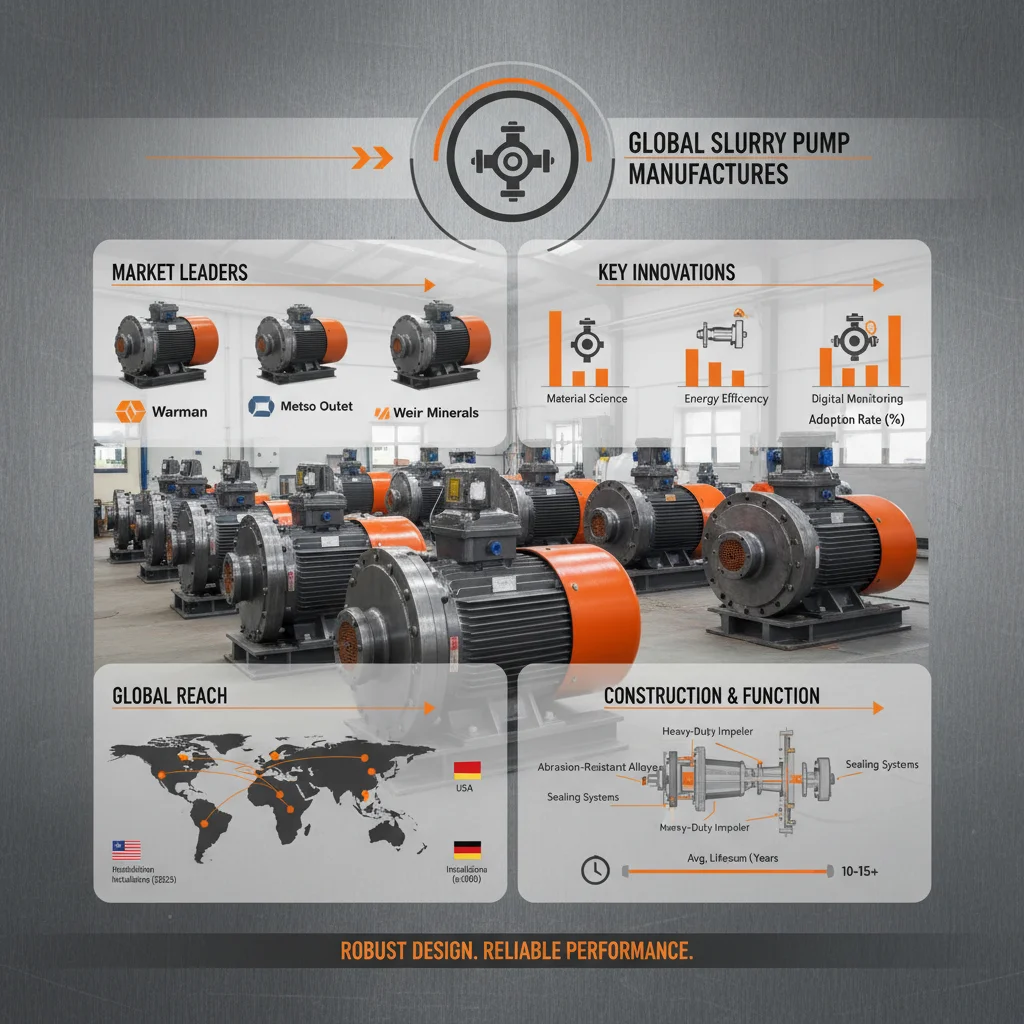
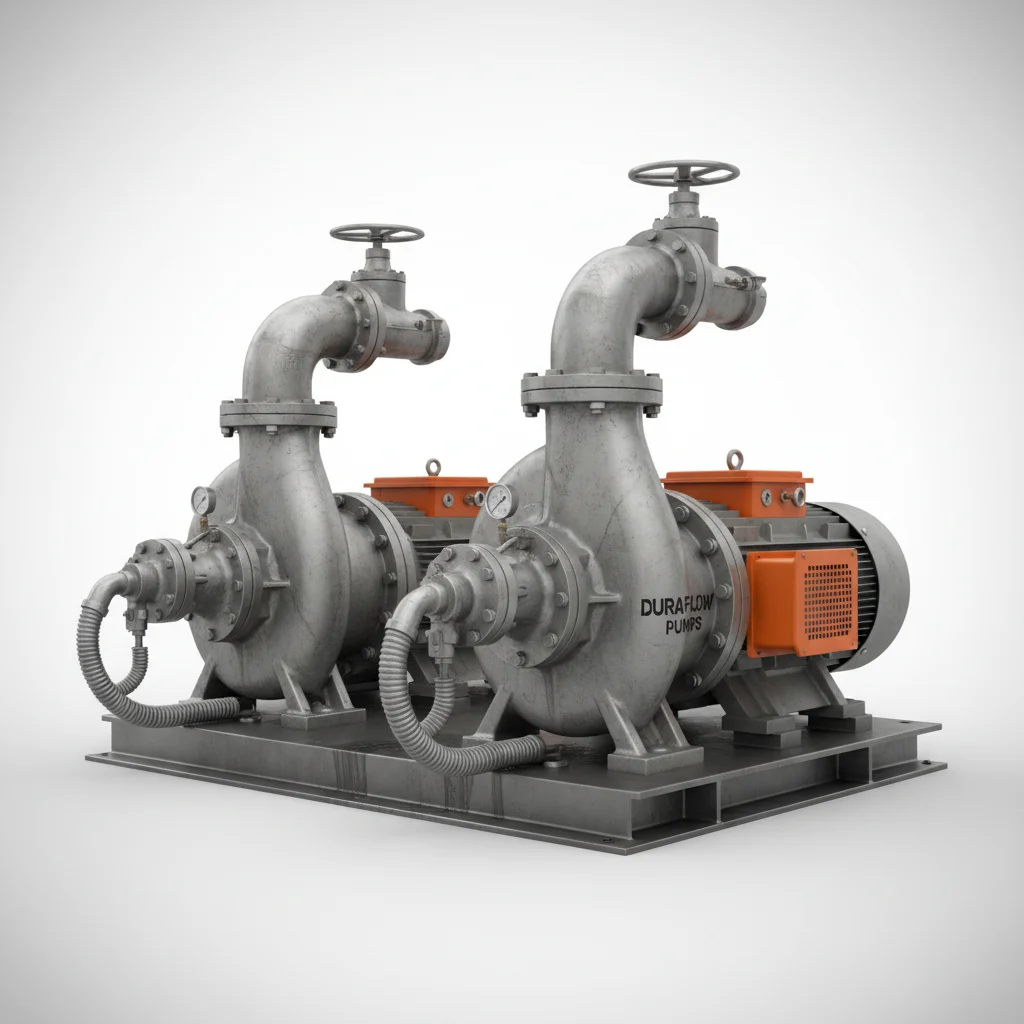
In the demanding world of mineral processing and metallurgy, the ability to move abrasive, dense fluids is a critical operational requirement. Heavy duty slurry pumps are the backbone of these industrial processes, designed to handle the extreme wear and tear caused by high concentrations of solid particles. Without specialized equipment, the abrasive nature of ore and tailings would lead to rapid system failure and costly downtime.
Globally, the mining sector faces increasing pressure to optimize efficiency while reducing total cost of ownership. This has led to a shift toward pumps that offer not just raw power, but precision engineering in materials science and fluid dynamics. The challenge lies in balancing the need for high flow rates and pressure with the necessity for extreme durability in the face of corrosive and abrasive media.
For enterprises operating in these harsh environments, investing in high-performance heavy duty slurry pumps ensures maximum operational stability and systemic efficiency. By utilizing advanced lining materials and robust casing designs, modern industrial pumps can now significantly extend their service life, ensuring that critical paths from hydrocyclone feed to tailings management remain uninterrupted.

Engineering Excellence of the HAH Series
The HAH series represents a pinnacle in the design of heavy duty slurry pumps, featuring a robust horizontal double-casing axial suction centrifugal architecture. This specific design is engineered for the continuous transportation of highly abrasive and dense slurries, providing a high-pressure solution that remains stable even under the most demanding mineral processing conditions.
By integrating a ductile iron fully lined casing, the HAH series ensures superior structural strength and safety. This prevents catastrophic casing failure during high-pressure operations, allowing the pump to maintain a flowrate range of 6.5 to 30,000 m³/h and a maximum head of 90m, making it one of the most versatile options for global industrial slurry requirements.
Core Components for Industrial Durability
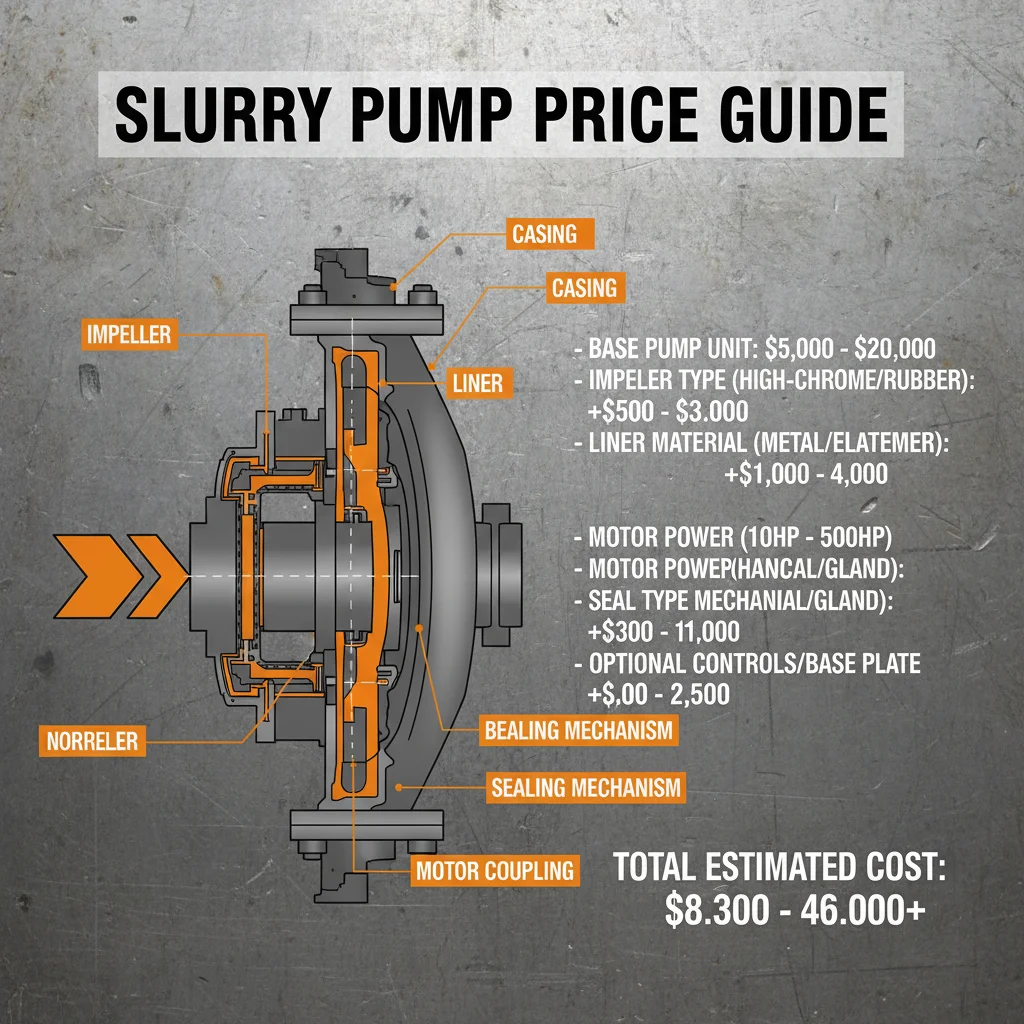
Durability in heavy duty slurry pumps is achieved through the synergy of high-grade materials and geometric optimization. The HAH series utilizes a ductile iron casing that is fully lined, which provides an essential barrier against the erosive forces of the medium. This ensures that the structural integrity of the pump is preserved over thousands of operating hours.
Another key factor is the flexibility of the outlet positioning. The design allows outlets to be positioned in 8 different directions at 45° intervals. This feature is not merely a convenience but a strategic advantage that optimizes plant piping layout and significantly reduces installation costs by minimizing the need for complex elbow joints.
Furthermore, the integration of versatile sealing systems and a wide variety of impellers ensures leak-proof operation. Whether dealing with high-viscosity fluids or high-velocity abrasive streams, these components are precision-matched to the specific requirements of the medium, reducing the risk of unplanned operational downtime.
Material Selection for Abrasive Media
Selecting the right liner material is the most critical decision when deploying heavy duty slurry pumps. The HAH series offers interchangeable linings, allowing operators to switch between high chrome alloy and rubber based on the specific nature of the slurry being transported.
High chrome alloy is the preferred choice for heavy duty slurry pumps handling sharp, highly abrasive particles, as its extreme hardness resists surface cutting. In contrast, rubber lining is ideal for softer, abrasive slurries and provides superior corrosion resistance, making it a versatile option for varied chemical environments.
This interchangeability ensures that the pump can adapt to varying slurry characteristics and wear rates without requiring a complete equipment replacement. This adaptive approach maximizes the lifespan of the wetted parts and optimizes the replacement cycle for liners and throat bushes.
Operational Performance and Pressure Capability
Performance in slurry handling is defined by the balance between flowrate and head pressure. While the standard HAH model is exceptionally capable, the HH variant is specifically optimized for high-density slurry applications that require even higher discharge pressure. This ensures that dense tailings or concentrated ores can be moved across long distances without settling.
The ability to customize impeller configurations allows plant managers to tune the pump for the optimal balance of head and flowrate. This precision tuning is essential for maintaining the stability of hydrocyclone feeds and flotation circuits, where consistent pressure is paramount for process efficiency.
Performance Rating of HAH Series Heavy Duty Slurry Pumps
Global Applications in Mining and Metallurgy
The application of heavy duty slurry pumps spans the globe, from the massive copper mines of Chile to the coal power plants of Asia. In these settings, the HAH series is primarily utilized for hydrocyclone feed, flotation, and the critical management of nonferrous mine tailings.
Beyond large-scale mining, these pumps are indispensable in metallurgy and coal processing. Their ability to handle high-concentration abrasive slurry makes them the ideal choice for transporting waste materials to tailings dams or moving raw ore through crushing and grinding circuits, ensuring that the entire production chain remains fluid.
Maintenance Efficiency and Lifecycle Value
One of the most significant costs in slurry handling is unplanned downtime. The HAH series addresses this through dual lubrication options—grease and oil lubrication. This flexibility allows maintenance teams to choose the system that best fits their operational environment, simplifying bearing maintenance and drastically reducing the frequency of emergency repairs.
Furthermore, the inclusion of simplified inspection ports allows for real-time wear monitoring of liners. Instead of guessing when a part might fail, operators can precisely track the erosion of the high chrome alloy or rubber linings and schedule replacements during planned shutdowns.
The availability of OEM-standard spare parts, including volute liners, throat bushes, and impellers, ensures that restoration of plant operations is rapid. By syncing spare parts procurement with wear monitoring, plants can maintain peak performance without overstocking expensive components.
Investment Return and TCO Analysis
When analyzing the Total Cost of Ownership (TCO), the initial purchase price of heavy duty slurry pumps is often eclipsed by the costs of maintenance and energy. Standard centrifugal pumps often fail quickly in abrasive conditions, leading to a cycle of frequent liner changes and high labor costs.
The HAH series is engineered to break this cycle. By utilizing ductile iron casings and superior lining materials, the wear life is significantly extended. This translates to fewer shutdowns and a lower overall cost per ton of material moved, providing a clear economic advantage over less robust alternatives.
Additionally, the flexible installation options reduce the initial piping investment. By optimizing the plant layout through the 8-way outlet positioning, companies can reduce the amount of steel piping required, contributing to a lower capital expenditure (CAPEX) and a faster return on investment.
Investment Return Comparison: Standard Pumps vs. HAH Heavy Duty Pumps
| Performance Indicator |
Standard Centrifugal Pump |
HAH Heavy Duty Pump |
Economic Impact |
| Wear Life |
Low (Frequent Changes) |
High (Chrome/Rubber) |
Reduced Labor Cost |
| Operational Uptime |
Moderate |
Maximum |
Higher Production Volume |
| Slurry Concentration |
Thin Slurries Only |
Optimized for Dense |
Improved Process Flow |
| Installation Cost |
Standard Piping |
Reduced (8-Way) |
Lower CAPEX |
| Maintenance Frequency |
High |
Low (Optimized) |
Lower OPEX |
| Total Cost (TCO) |
Higher (Replacement) |
Lower (Lifecycle) |
Increased Profitability |
FAQS
While both are heavy-duty, the HH series is specifically designed for higher-density slurry applications and can operate under significantly higher pressure conditions than the HAH series. This makes the HH variant better suited for extreme tailings management where higher discharge pressure is required to move thick materials.
The choice depends on the medium's characteristics. High chrome alloy is recommended for sharp, highly abrasive particles that would cut through rubber. Rubber lining is ideal for softer, abrasive slurries and provides excellent corrosion resistance, making it a cost-effective choice for less aggressive solids.
The pump is designed to allow the outlet to be positioned in 8 different directions (every 45°) during the setup process. This allows you to fit the pump perfectly into your specific plant layout to optimize piping and space, though it is intended to be configured during installation.
They are widely used in mineral processing, metallurgy, coal power plants, and nonferrous mine tailings management. Any industrial process that requires the continuous transport of high-concentration abrasive slurry can benefit from the durability of the HAH series.
The HAH series offers both grease and oil lubrication options. Regular lubrication according to the provided manual is essential to minimize friction and extend bearing life. The dual options simplify maintenance and help reduce unplanned downtime.
Yes, we provide a full range of OEM spare parts, including volute liners, throat bushes, frame plate liner inserts, and impellers. Using OEM parts ensures that the pump maintains its original performance specifications and extends the overall operational life.
Conclusion
The implementation of heavy duty slurry pumps like the HAH series is a strategic necessity for any high-output mineral processing or metallurgical operation. By combining ductile iron structural strength with interchangeable high chrome or rubber linings, these pumps effectively mitigate the extreme wear associated with abrasive slurries. The ability to optimize flowrate, head pressure, and piping layout ensures that systemic efficiency is maximized while the Total Cost of Ownership is minimized.
Looking forward, the trend toward higher slurry concentrations and more remote mining sites will only increase the demand for pumps that offer extreme reliability and ease of maintenance. For operators seeking to enhance their operational uptime and reduce lifecycle costs, the HAH series provides a proven, scalable solution. We invite you to visit our website at www.hihornpump.com to find the perfect configuration for your industrial slurry handling needs.