In the demanding landscape of mineral processing, the efficiency of fluid and froth transport is paramount to operational success. Managing abrasive slurries and thick foams requires specialized equipment designed to handle high solids concentrations without succumbing to premature wear or air-lock issues. Understanding the role of a sumpit pump—specifically within the context of froth and slurry management—is essential for engineers aiming to optimize flotation processes and reduce downtime.
Globally, the mining and mineral industries face increasing pressure to process lower-grade ores, which necessitates higher throughput and more robust pumping solutions. The challenge lies in transporting "froth slurry," a complex mixture of air bubbles and mineral particles that can easily cause cavitation or loss of prime in standard pumping systems. This technical hurdle requires a shift toward specialized vertical designs that can actively eliminate foam while maintaining a steady flow of abrasive material.
The HAF Series Vertical Froth Pump represents a pinnacle in this engineering niche, offering a double pump shell structure that ensures durability and operational stability. By integrating semi-open impellers and a versatile hopper feeding box, this sumpit pump equivalent for froth applications eliminates the need for shaft seals and manages air-heavy slurries with ease. Whether dealing with high-chromium requirements or rubber-lined protection, these systems are built to sustain the rigors of industrial mineral processing.

Engineering Design of Froth Slurry Systems
The engineering behind the HAF Series is centered on a double pump shell structure, which provides a robust foundation for handling the volatile nature of froth slurries. Unlike traditional pumping setups, this design focuses on a vertical orientation that utilizes gravity and specialized impeller geometry to manage the air-liquid interface. The semi-open impeller, featuring vanes on the top or both sides, is specifically engineered to prevent the air-locking that typically plagues a standard sumpit pump when dealing with flotation froth.
Furthermore, the inclusion of a steel plate hopper feeding box adds a layer of versatility. This box can be lined based on the specific abrasive characteristics of the conveying media, ensuring that the entry point of the slurry is as protected as the internal pump components. With the ability to change the outlet position at 45-degree intervals, the system offers unparalleled flexibility for plant layout integration, ensuring the froth slurry is directed efficiently to the next stage of processing.
Material Durability and Wear Resistance
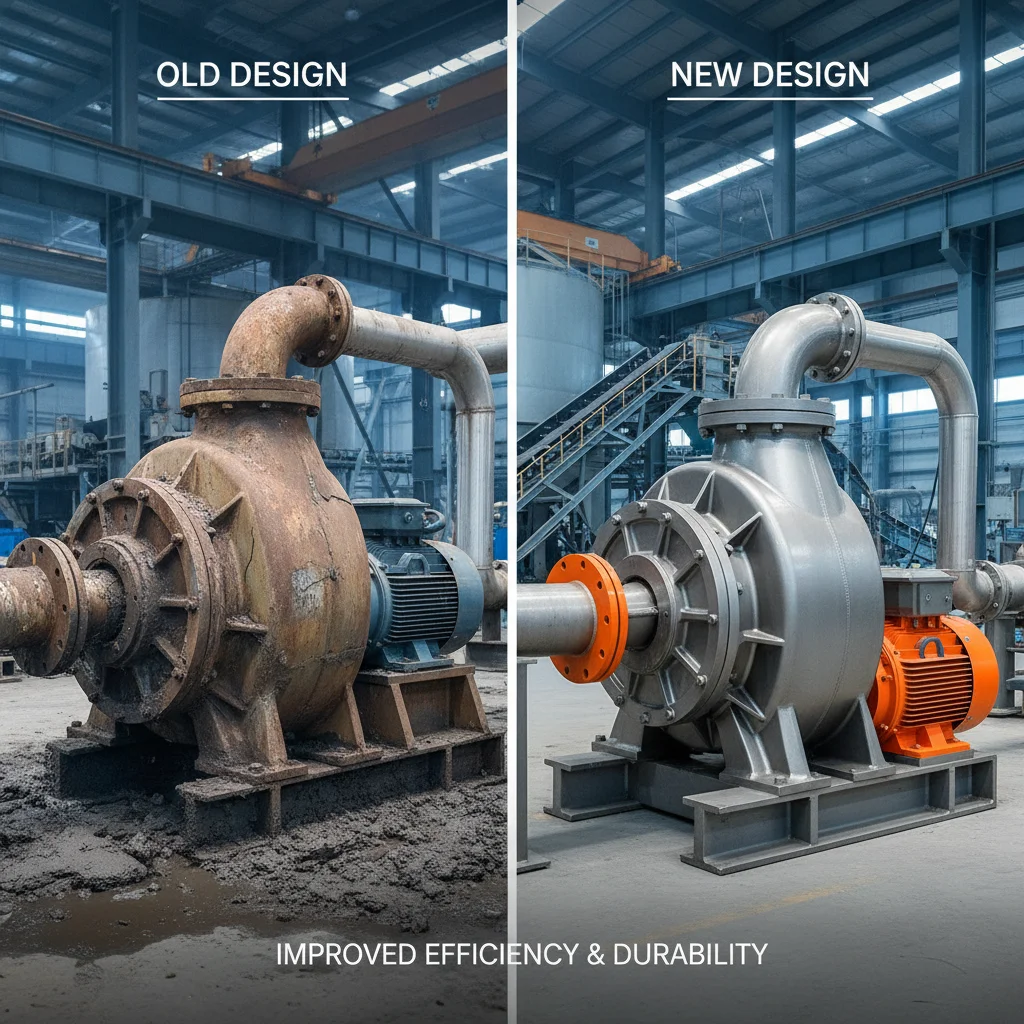
In the world of abrasive slurry transport, material selection is the primary determinant of equipment lifespan. The HAF Series employs high-performance materials including hard nickel, high chromium, and specialized rubber. These materials are chosen based on the chemical composition and particle size of the slurry, ensuring that the flow parts can withstand the constant scouring action of mineral particles.
The decision to omit shaft seals in this specific vertical design is a strategic engineering choice. By removing a common point of failure, the pump minimizes the risk of leakage and reduces the frequency of costly maintenance interventions. This makes the system significantly more reliable than a conventional sumpit pump when exposed to the highly corrosive and abrasive environments found in mineral processing plants.
Rubber lining is particularly effective for slurries with high elastic impact or corrosive elements, while high chromium alloys are preferred for high-pressure, high-wear applications. This modular approach to material selection allows operators to customize their equipment to the specific ore body they are mining, maximizing the interval between overhauls and reducing the total cost of ownership.
Operational Mechanisms for Foam Elimination
One of the most critical challenges in flotation processes is the accumulation of foam, which can displace liquid and lead to pump cavitation. The HAF Series solves this through a specialized vertical design that effectively eliminates foam during operation. This ensures that the sumpit pump maintains a consistent prime and does not suffer from the efficiency drops associated with air-entrained fluids.
A key operational advantage is the pump's ability to work normally even when the incoming material is insufficient. This "low-feed" stability is vital in intermittent processing cycles, where the flow of froth slurry may fluctuate. By maintaining a stable hydraulic environment, the pump prevents the surging and vibration that can damage piping and supporting structures.
When compared to horizontal slurry pumps used for mineral froth, the vertical HAF series is often more compact for the same capacity. However, it is important to note that horizontal variants are typically used when significantly larger flow rates are required. For most flotation cells, the vertical sumpit pump configuration provides the optimal balance of footprint and foam-handling capability.
Performance Analysis and Flow Capacity
The performance metrics of the HAF series are designed to scale with the size of the industrial operation. With discharge diameters ranging from 50mm to 550mm, these pumps can handle flow rates of up to 11,400 m³/h and reach a maximum head of 80m. This wide range ensures that whether a small-scale pilot plant or a massive global mining operation is in need, there is a configuration that matches the hydraulic requirements.
Efficiency is closely tied to the model selection and the concentration of the slurry. For instance, the HAF-3 and HAF-4 models exhibit peak efficiencies of around 55%, making them highly effective for medium-scale froth transport. The following chart illustrates how different configurations of our sumpit pump technology perform across various efficiency and power benchmarks.
Performance Comparison of HAF Series Configurations
Global Industrial Applications
The application of this specialized sumpit pump technology spans across diverse geographical regions, from the copper mines of Chile to the gold processing plants in Australia. In these environments, the ability to handle abrasive slurry with high concentration is not just a preference but a requirement for operational viability. The HAF Series is particularly indispensable in the flotation stage, where mineral-rich froth must be moved quickly to thickeners or filter presses.
Beyond traditional mining, these pumps find use in industrial chemical processing and waste management where air-entrained abrasive liquids are common. In remote industrial zones, the low-maintenance nature of the seal-less design reduces the reliance on highly specialized on-site technicians, allowing for more sustainable and autonomous operation in challenging terrains.
Long-term Value and Maintenance
Investing in high-grade froth pumps yields long-term dividends through the reduction of unplanned downtime. The ability to customize the lining of the hopper and the selection of flow-part materials means that the equipment evolves with the mine's life cycle. As ore hardness changes over the years, the sumpit pump components can be replaced with materials that better suit the new conditions without replacing the entire pump structure.
From a financial perspective, the increased efficiency and reduced wear lead to lower energy costs per ton of material moved. The HAF series' capacity to eliminate foam effectively prevents the energy waste associated with pumping air, ensuring that every kilowatt of power is used to move actual mineral slurry. This logical approach to efficiency translates directly into improved profit margins for mining enterprises.
Moreover, the emotional peace of mind provided by a reliable system cannot be overstated. In high-pressure production environments, the trust that a pump will not fail during a peak production cycle allows managers to focus on optimization rather than crisis management. This reliability fosters a culture of innovation and stability within the plant's operational framework.
Future Trends in Pumping Technology
The future of slurry and froth transport is moving toward greater integration with digital transformation and automation. We are seeing a shift toward "smart" sumpit pump systems that utilize IoT sensors to monitor wear in real-time. By analyzing vibration and flow patterns, these systems can predict exactly when a liner needs replacing, moving the industry from reactive to predictive maintenance.
Sustainability is another driving force. The development of new, eco-friendly elastomers and recycled high-chromium alloys is reducing the environmental footprint of pump manufacturing. Furthermore, the integration of variable frequency drives (VFDs) allows pumps to adjust their flow rate in real-time based on the incoming froth volume, significantly reducing carbon emissions associated with energy over-consumption.
As the industry moves toward deeper mines and more complex mineralogy, the demand for pumps that can handle extreme pressures and highly corrosive media will grow. The evolution of the HAF series will likely include advanced computational fluid dynamics (CFD) to further optimize impeller vanes, ensuring that foam elimination becomes even more efficient, further cementing the role of the specialized sumpit pump in the modern industrial era.
Technical Specifications and Performance Matrix of HAF Series
| Model Variant |
Max Flowrate (m³/h) |
Max Head (m) |
Efficiency Score (1-10) |
| HAF-2Q |
335 |
30 |
7 |
| HAF-3Q |
104 |
28 |
9 |
| HAF-4R |
130 |
28 |
8 |
| HAF-6S |
330 |
25 |
10 |
| HAF-8S |
425 |
30 |
7 |
| Custom OEM |
11400 |
80 |
9 |
FAQS
A standard pump often struggles with air-locking when handling froth, leading to cavitation and loss of prime. The HAF Series vertical froth pump is specifically engineered with a double shell structure and semi-open impellers that actively eliminate foam, ensuring a steady flow of slurry even with high air content.
Yes. By utilizing high chromium, hard nickel, or rubber linings for the flow parts and the hopper feeding box, these pumps are designed to resist the scouring action of abrasive mineral slurries. The absence of shaft seals further removes a primary point of failure common in other pumps.
The HAF Series is designed to work normally even when the incoming material is insufficient. Its unique hydraulic design prevents the surging and instability that usually occur in conventional pumps during low-feed periods, maintaining operational continuity.
The series is highly scalable, with discharge diameters ranging from 50mm up to 550mm. In its largest configurations, it can handle flow rates up to 11,400 m³/h and reach a maximum head of 80 meters, making it suitable for the largest global mining operations.
Yes, the design allows the pump outlet position to be changed at 45-degree intervals. This provides significant flexibility for engineers to optimize the piping layout and integrate the pump into existing plant infrastructure without needing complex adapters.
Rubber is ideal for slurries with high corrosive properties or those that cause elastic impact wear. High chromium alloys are better suited for extremely abrasive, high-pressure environments where hardness is the primary requirement for longevity.
Conclusion
In summary, the management of mineral froth and abrasive slurries requires a departure from conventional pumping logic. The HAF Series Vertical Froth Pump addresses the core challenges of foam elimination, material wear, and operational stability through its innovative double shell structure and seal-less design. By prioritizing material durability and hydraulic efficiency, this specialized sumpit pump alternative ensures that mineral processing plants can maintain high throughput with minimal maintenance overhead.
Looking forward, the integration of smart monitoring and sustainable materials will further enhance the value of these systems. For operators seeking to optimize their flotation circuits and reduce total cost of ownership, investing in a purpose-built froth pumping solution is the most strategic path toward operational excellence. Visit our website for more professional slurry solutions: www.hihornpump.com